Views: 0 Author: Site Editor Publish Time: 2026-10-05 Origin: Site
Processing fine and micro denier fibers presents a unique engineering challenge on the production floor. Standard specifications fail when applied to these delicate materials. Improper cut lengths immediately lead to severe production bottlenecks. You will experience machine jamming, excessive nep formation, poor fiber opening, and compromised end-product loft. Mismatching cut length with fine denier specifications introduces significant operational risks. It disrupts workflow and degrades the final product quality.
This guide provides a technical framework for operations managers and procurement teams. It helps you evaluate, shortlist, and match the correct cut length to your specific machinery. We analyze the mechanical relationship between fiber diameter and length. You will learn how varying lengths interact with fiber tenacity, processing equipment, and final application goals. Understanding these variables ensures optimal processing efficiency and superior product performance.
Equipment Dictates Length: The primary constraint for cut length selection is the opening and carding equipment; high-speed blowing machines typically require shorter lengths (25mm–32mm) to prevent tangling.
The Denier-to-Length Ratio: As denier decreases (becoming finer), the optimal cut length often must decrease proportionally to maintain drafting uniformity and prevent fiber breakage.
Crimp and Tenacity Variables: Cut length cannot be evaluated in a vacuum; it must align with the fiber's Crimp per Inch (CPI) and tenacity (typically 2.5 to 5.5 grams per denier for fine fibers) to ensure structural integrity during processing.
End-Product Performance: Shorter cut lengths maximize the ultra-soft, down-like feel of micro denier fibers, while longer lengths (51mm–64mm) are necessary for structural cohesion in batted or high-bulk applications.
Risk of Neps: Selecting a cut length that is too long for a fine denier fiber exponentially increases the risk of nep formation (small, tangled knots) during the carding process.
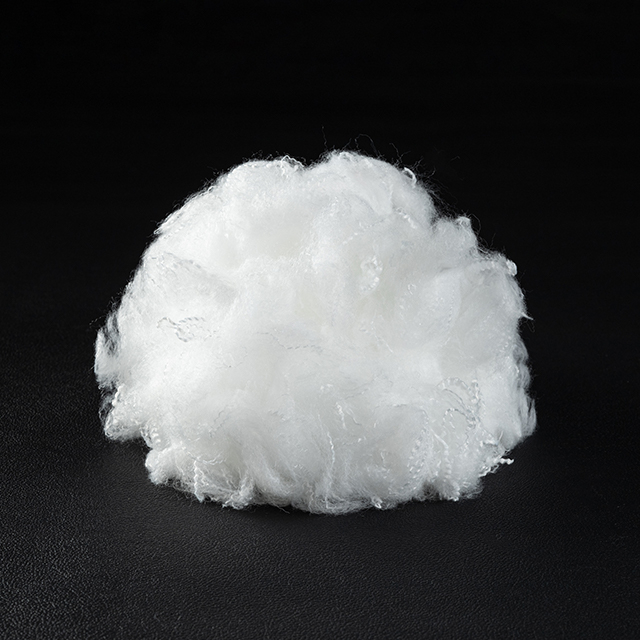
Defining the exact parameters of fine denier is the first step in optimizing production. Fine denier generally falls under 3D in thickness. A true micro denier polyester fiber typically ranges from 0.7D to 1.5D. These ultra-thin dimensions fundamentally alter how the material behaves under mechanical stress. You cannot treat these fibers like standard coarse materials. Their structural properties demand specific handling protocols during opening and carding.
We must explicitly contrast the mechanical behavior of fine fibers with standard 7D or 15D Hollow Conjugated Fiber (HCS). Standard HCS thrives at 64mm lengths. The thicker diameter provides rigidity. This rigidity allows the fiber to maintain maximum loft without collapsing. Applying those same 64mm dimensions to microfibers causes catastrophic entanglement. Fine fibers lack the structural backbone to support long cut lengths during aggressive processing. They fold, twist, and knot together almost instantly when subjected to high-speed drafting.
The mechanical relationship between fiber diameter and length directly impacts fiber cohesion and drafting. Finer fibers possess significantly more surface area per unit of weight. This increased surface area exponentially increases friction between individual strands. High friction alters how fibers draft and separate during processing. When processing Fine Denier Polyester Staple Fiber, you must account for this friction. Shorter cut lengths reduce the contact area between fibers, facilitating smoother separation and preventing the formation of dense clumps.
Mechanical strength and crimp frequency dictate the maximum viable cut length. Tenacity measures this strength, typically falling between 2.5 to 5.5 grams per denier for fine fibers. Crimp per Inch (CPI) measures the wave frequency along the fiber shaft. High CPI increases cohesion but also increases the risk of tangling. You must balance tenacity and CPI against the cut length. Aggressive carding will break weak, excessively long fibers. This breakage generates dust, clogs extraction systems, and degrades the final product quality.
Static electricity generation presents another physical hurdle on the factory floor. Fine fibers generate massive static charges due to their high surface area and constant friction against metal machine parts. Longer cut lengths exacerbate this issue by increasing the duration of metal-to-fiber contact. High static charges cause the fibers to cling to the main cylinder and doffer wires, resisting transfer and causing severe pill-ups. Shorter cut lengths minimize this contact time, reducing static buildup and allowing for cleaner fiber transfer between carding components.
Establishing success criteria for fiber selection ensures consistent production outcomes. A successful specification yields zero machine downtime. It achieves an optimal opening rate, maximizing material yield. You must observe consistent web uniformity without thin spots or heavy clumps. Finally, the processed fiber must deliver the target tactile properties. It should provide the exact softness, recovery, and thermal insulation required for the final application.
The 25mm to 32mm range serves as the industry standard for most automated stuffing machines. Fine-opening carding lines rely heavily on these shorter lengths. Shorter fibers navigate pneumatic transport systems with ease. They prevent clogging in narrow transport tubes and blower nozzles. This length range ensures drafting uniformity across high-speed production lines. It allows for rapid, individualized separation of the fiber strands without inducing mechanical stress.
Utilizing these shorter lengths delivers specific, highly desirable outcomes. Rapid separation produces a premium micro down filling fiber feel. The fibers move independently within the final product casing. This independent movement mimics natural goose down. It creates an ultra-soft, luxurious tactile experience. Shorter lengths maximize processing speed while minimizing the risk of mechanical jams, allowing operators to run blowing lines at maximum RPM.
Operators must calibrate their fine-opening machines specifically for this length. The clearance between the feed roller and the licker-in must be tightened. If the gap remains set for standard 64mm fibers, the 32mm strands will slip through unopened. This slippage results in dense, unyielding lumps in the final product. Precision calibration ensures every individual fiber separates, maximizing the volumetric yield of the raw material.
Mid-range lengths between 38mm and 51mm offer a versatile middle ground for specific applications. Nonwoven applications frequently utilize these lengths. Certain pillow filling lines that balance blowing with light carding also benefit from this range. These lengths provide enough structural hold to form cohesive webs. They bridge the gap between loose fill and continuous batting, offering a hybrid solution for manufacturers producing diverse product lines.
Choosing this middle ground involves a calculated trade-off. You gain improved structural integrity and web cohesion. The fibers interlock more effectively, preventing migration within the casing. However, this comes at the slight expense of maximum processing speed. You also sacrifice a small degree of ultimate softness. The fibers cannot move as independently as the 32mm variants, resulting in a slightly firmer hand feel.
Processing 51mm fine denier requires specific airflow management. The extended length increases the drag coefficient within pneumatic transport tubes. You must increase the blower fan RPM to maintain adequate transport velocity. Failing to adjust the airflow will cause the fibers to settle and accumulate at the bottom of horizontal ducting runs, eventually leading to a complete blockage.
Evaluating 64mm fine denier fibers reveals highly limited but specific use cases. Specialized high-bulk carding lines producing continuous batting occasionally utilize this length. These lines operate at slower speeds with highly calibrated wire clothing. The extended length provides maximum tensile strength for batted products. It ensures the batting holds together during subsequent manufacturing steps, such as quilting or foam wrapping.
Implementing 64mm or 76mm lengths carries severe risks in standard equipment. The 76mm length is generally reserved strictly for coarse fibers. Attempting to process 76mm micro denier will cause immediate machine failure. Standard blowing equipment cannot handle the extreme friction and tangling. You will experience massive nep formation, pneumatic bridging, and total line shutdown within minutes of starting the feed.
If a specific application absolutely demands a 64mm fine denier, you must drastically reduce production speeds. The main cylinder RPM must drop by at least 30% compared to standard processing parameters. This speed reduction minimizes the centrifugal force and mechanical tearing applied to the long, delicate strands. You must also apply heavy anti-static conditioning sprays to the fiber bales prior to processing to mitigate the massive friction generated by the extended length.
Auditing your current equipment is mandatory before selecting a cut length. You must measure nozzle diameters on all stuffing machines. Evaluate the air pressure capacities of your pneumatic blowers. Document the maximum feed rates your system can sustain without choking. These physical constraints dictate the absolute maximum cut length your line can process safely.
Calculating the maximum allowable cut length prevents pneumatic bridging. Bridging occurs when long fibers interlock across the diameter of a transport tube. This creates a solid plug that blocks airflow. Finer deniers require shorter lengths to prevent this interlocking. If your nozzle diameter is narrow (under 50mm), you must strictly adhere to 25mm or 32mm lengths to maintain continuous operation and prevent costly downtime.
The internal surface finish of your ducting also plays a role. Rough internal welds or sharp bends in the pneumatic transport system will catch longer fine denier fibers. A 32mm fiber might navigate a 90-degree elbow smoothly, while a 51mm fiber will snag, accumulate, and block the pipe. Inspect your entire transport line and replace any corrugated or rough-walled ducting with smooth, polished stainless steel pipes.
Wire clothing specifications heavily impact the processing of fine fibers. The teeth per inch (TPI) on the main cylinder must match the fiber denier. Fine fibers require higher TPI to ensure individual separation. The Crimp per Inch (CPI) interacts directly with these wires. High CPI fibers grip the wires tightly, requiring precise speed adjustments to prevent breakage and dust generation.
Cut length significantly affects the transfer efficiency between the cylinder and the doffer. Shorter lengths require tighter gauge settings between these components. If the gap is too wide, short fibers will drop out as waste beneath the machine. If the gap is too tight, the fibers will grind and break against the metal. Calibrating these settings based on the exact cut length ensures maximum yield and web uniformity.
The worker and stripper rollers must also be adjusted for fine denier processing. When running 32mm lengths, the worker rollers need to be set closer to the main cylinder to catch and open the short clumps effectively. If you switch to a 51mm length, you must back these rollers off slightly. Failing to increase the clearance for longer fibers will result in over-carding, which destroys the fiber's natural crimp and ruins its lofting ability.
Nep formation stands as the primary risk when processing long, fine fibers. Neps are small, tightly tangled knots of fiber. They occur when equipment over-processes delicate strands. Long microfibers wrap around carding wires or tangle in turbulent airflows. Once formed, neps are impossible to remove. They create hard lumps in the final product, destroying the desired soft texture and causing the product to fail quality control inspections.
Implementing strict mitigation strategies protects your production line. Adjust machine speeds to reduce mechanical stress on the fibers. Utilize fibers treated with high-quality anti-static finishes to reduce friction. Implement strict humidity controls on the production floor. Maintaining optimal ambient humidity (typically between 65% and 70% RH) prevents static buildup, which is a major catalyst for fiber tangling and nep formation.
Cut Length Range | Ideal Denier Match | Primary Equipment Compatibility | Optimal End-Product Application | Primary Risk Factor |
|---|---|---|---|---|
25mm - 32mm | 0.7D - 1.5D | High-speed pneumatic blowers, fine-opening lines | Sleeping pillows, apparel insulation (baffles) | Drafting dropout if gauge settings are too wide |
38mm - 51mm | 1.2D - 3.0D | Light carding lines, specialized blowers | Decorative cushions, nonwoven textiles | Slight reduction in ultimate down-like softness |
64mm - 76mm | 3.0D and above | High-bulk continuous carding lines | Upholstery batting, mattress pads | Severe nep formation and machine jamming if used with micro denier |
When neps appear in the output web, you must halt production immediately to diagnose the root cause. Neps in fine denier processing usually indicate a mismatch between the cut length and the cylinder speed. If you are running a 51mm fiber and observing neps, your main cylinder is likely spinning too fast. The excessive speed creates aerodynamic turbulence that whips the long, flexible ends of the fibers into knots before they can transfer to the doffer.
To resolve this, reduce the main cylinder RPM in 5% increments until the nep formation ceases. If speed reduction fails, inspect the wire clothing on the worker rollers. Dull or damaged wires will fail to separate the fibers cleanly, dragging them into tangled clumps. Fine denier fibers require exceptionally sharp, well-maintained wire clothing to process cleanly without nepping.
Static electricity acts as an invisible barrier to efficient fine fiber processing. When processing 32mm micro denier, static causes the short fibers to fly erratically off the doffer comb, creating a messy, uneven web. The fibers will cling to the metal side frames of the carding machine, accumulating until they fall into the web as dense, unopened slugs.
You must attack static at the environmental level. Install overhead humidification systems directly above the opening and carding lines. Target a relative humidity of 65% to 70%. If environmental controls are insufficient, you must apply an anti-static overspray directly to the fiber bales as they enter the bale breaker. Ensure the overspray is compatible with the fiber's existing silicone finish to prevent chemical degradation.
Pneumatic transport systems require precise air-to-fiber ratios to function correctly. If you feed 32mm fine denier into a blower with insufficient airflow, the fibers will drop out of suspension and clog the pipes. Conversely, if the airflow is too high, the turbulent air will spin the fibers into tight, rope-like structures known as "pigtails."
You must calibrate the blower fan speed to match the specific weight and length of the fiber. Fine denier fibers are incredibly light and require less aggressive airflow than coarse fibers. Install variable frequency drives (VFDs) on all transport fans. This allows operators to dial in the exact air velocity required to keep the 32mm or 51mm fibers suspended smoothly in the center of the ducting without inducing turbulent tangling.
Sleeping pillows demand specific tactile properties to ensure user comfort. Ultra-fine denier paired with shorter cut lengths is critical for this application. A 0.9D x 32mm specification replicates the slick, independent movement of natural goose down. The short fibers slide past each other under pressure. This allows the pillow to conform perfectly to the user's head and neck without creating pressure points.
Decorative throw pillows require entirely different mechanical properties. These cushions need structural hold to maintain their shape on a sofa. They benefit from a 51mm cut length. The longer fibers interlock, providing resistance against compression. Alternatively, blending fine denier with coarser fibers achieves the necessary rigidity while maintaining a soft surface feel. The 51mm length ensures the pillow stands upright and fills out the corners of the fabric casing.
Baffled jackets and outerwear require highly specialized insulation materials. You need a soft polyester filling fiber that can be injected into extremely small compartments. Short cut lengths (25mm to 32mm) are mandatory here. They flow smoothly through small injection nozzles without clumping. This ensures even distribution throughout the baffle, preventing the insulation from bunching at the seams.
Even distribution prevents the formation of cold spots in the garment. If fibers clump due to excessive length, voids appear in the insulation layer. Short, fine fibers expand uniformly to fill the available space. They trap maximum air volume, providing superior thermal insulation while maintaining a lightweight, compressible profile. This compressibility allows the garment to be packed tightly without damaging the internal fiber structure.
Upholstery applications often utilize wrapped cushions for seating. These scenarios require a slightly longer cut length, typically between 51mm and 64mm. The fiber must form a cohesive batting that wraps around a foam core. Short fibers would simply fall apart during the wrapping process. The longer length provides the necessary tensile strength to hold the batting together as it is stretched over the foam.
Tensile strength prevents the fiber from migrating through the upholstery fabric over time. Long fibers anchor themselves within the batting structure. They resist the constant friction and compression of daily use. This structural integrity extends the lifespan of the furniture, maintaining a smooth, even appearance on the cushion surface and preventing the fabric from wrinkling or sagging.
Maximizing softness inherently reduces structural resilience. Finer, shorter fibers provide an incredibly soft hand feel. However, they lack the mechanical memory to spring back after heavy compression. Thicker, longer fibers offer superior loft recovery. You must balance this trade-off based on the specific performance requirements of your end product.
Understanding this conceptual trade-off guides procurement decisions. If the product requires high resilience, you cannot rely solely on micro denier short-cut fibers. You must adjust the denier upwards or blend with longer lengths. Conversely, if ultimate softness is the only metric that matters, you must accept lower structural resilience and design the product casing accordingly, perhaps by overstuffing the casing to compensate for the lack of mechanical spring.
Shorter cut lengths often require more precise opening equipment. High-precision carding and blowing lines demand strict maintenance schedules. Calibrating these machines for micro fibers can slow overall throughput. Slower processing speeds directly impact operational costs. You must factor these processing variables into your production scalability models to ensure profitable manufacturing runs.
Scaling production with fine denier fibers requires careful planning. You cannot simply increase feed rates to boost output. Pushing equipment past its optimal speed limits with fine fibers guarantees nep formation and machine jamming. Scalability relies on optimizing machine settings, maintaining consistent environmental controls, and ensuring the raw material specifications perfectly match the equipment capabilities.
Selecting the correct cut length minimizes un-opened fiber waste. Un-opened fibers form dense "pill-ups" that must be discarded. This waste represents a direct loss of purchased raw material. Proper cut length ensures maximum opening efficiency. Every kilogram of raw fiber translates into usable, high-loft filling material, directly improving the bottom line of the manufacturing operation.
Product uniformity across production batches relies on consistent fiber processing. The right cut length guarantees even drafting and predictable volumetric yield. You can accurately calculate the exact weight of fiber required to fill a specific volume. This precision reduces over-filling, controls material costs, and ensures every product meets strict quality assurance standards before shipping to the end user.
Machine Component | Setting for 32mm Fine Denier | Setting for 51mm Fine Denier | Operational Impact |
|---|---|---|---|
Main Cylinder RPM | High (Standard) | Reduced by 15-20% | Prevents aerodynamic tangling of longer fibers. |
Worker Roller Clearance | Tight Gauge | Medium Gauge | Ensures proper opening without grinding or breaking the fiber. |
Blower Fan Velocity | Standard | Increased by 10-15% | Prevents longer fibers from settling in horizontal ducting. |
Doffer Comb Speed | Fast | Moderate | Maintains web integrity and prevents static fly-aways. |
Audit the maximum length capacity of your current opening and blowing equipment by measuring nozzle diameters and air pressure limits.
Define the exact target softness and structural cohesion required for your specific end product before ordering raw materials.
Select the corresponding denier-to-length ratio that satisfies both your equipment constraints and product performance goals.
Request Technical Data Sheets and order small-batch samples for trial runs on your specific machinery to verify drafting uniformity.
Consult with fiber engineers to verify that the crimp per inch and silicone finish align with your carding wire specifications.
A: The optimal cut length typically ranges from 25mm to 32mm. This short length ensures optimal opening and drafting uniformity in high-speed blowing machines. It prevents pneumatic clogging and allows the fine fibers to move independently. This perfectly replicates the luxurious, slick movement of natural goose down without causing machine jams.
A: Denier dictates the softness of the material, while cut length dictates its structural cohesion. A length that is too short reduces structural loft and resilience. A length that is too long causes severe clumping and nep formation. This completely destroys the fiber's ability to trap air and maintain consistent loft.
A: The thicker diameter and inherent rigidity of 7D or 15D fibers prevent tangling. This allows them to support 64mm lengths for maximum batting loft. Fine denier fibers lack this structural rigidity. They cannot support 64mm without severe entanglement and nep formation in standard high-speed processing equipment.
A: No. Using a 64mm fine denier fiber in a standard pneumatic blower carries a massive risk of machine jamming. The long, flexible fibers will interlock inside the transport tubes. This causes pneumatic bridging, severe nep formation, and immediate line shutdowns. You must stick to shorter lengths for blowing.
A: Neps result from a combination of fine denier, excessive cut length, high crimp per inch, and aggressive carding speeds. When long, delicate fibers face high mechanical friction or turbulent airflow, they wrap around equipment wires or each other. This forms permanent knots that ruin the final product texture.
A: A 32mm length is ideal for loose, blowable fill in sleeping pillows. It provides independent fiber movement and extreme softness. A 51mm length is better suited for carded, cohesive batting used in quilts and mattress pads. The longer length provides the structural hold required for these flat applications.
A: No. A silicone finish significantly affects the slickness, hand feel, and surface friction of the fiber. However, it does not change the fundamental mechanical length limits. Those limits are strictly dictated by your machinery's capabilities, nozzle diameters, and the inherent tenacity of the fiber itself.