Views: 0 Author: Site Editor Publish Time: 2026-09-10 Origin: Site
In thermal bonding processes, the melting point of the binder fiber dictates line speed, energy consumption, and the structural integrity of the final nonwoven fabric. Specifying an incorrect melting point results in costly production failures. You either face incomplete bonding, which causes delamination and poor tensile strength, or you trigger substrate degradation, leading to shrinkage, stiffening, and polymer breakdown. Selecting the optimal melting point requires aligning the thermal characteristics of the bonding fiber with your oven capabilities, substrate limitations, and end-use performance requirements. This guide breaks down the technical evaluation criteria for selecting the right melting point for your production line. We will examine core-sheath mechanics, substrate compatibility, and how physical fiber dynamics impact heat transfer in industrial ovens.
Core-Sheath Mechanics: The ideal melting point applies only to the sheath polymer, allowing it to flow and create bond points while the core remains intact to provide structural stability.
Substrate Compatibility: The melting point of the binder must be at least 20°C to 30°C lower than the melting point of the primary matrix fibers to prevent substrate deformation.
Application Specificity: Standard applications typically utilize 110°C melting points, while specialized industrial applications require 130°C to 180°C ranges for higher thermal stability.
Process Optimization: Lower melting points reduce energy consumption and increase potential line speeds, but may compromise the high-temperature resistance of the finished product.
Physical Fiber Dynamics: A fiber's denier directly impacts heat transfer; thicker fibers require more thermal energy or longer dwell times to achieve the same sheath melt flow as finer fibers.
A successful thermal bond relies on precise temperature control and polymer flow. Optimal tensile strength occurs when the binder polymer flows adequately to wrap around the matrix fibers at their intersection points. Capillary action draws the liquefied sheath material into these crossover junctions, creating a strong weld once cooled. Correct loft retention demands that the web does not collapse under thermal stress during this phase. Uniform fiber distribution prevents dense spots or weak zones that compromise the fabric's physical properties. If the temperature is too low, the polymer merely softens without adhering, resulting in a web that pulls apart easily. If the temperature is too high, the polymer liquefies completely, wicking away from the intersections and causing severe thermal shrinkage across the entire web.
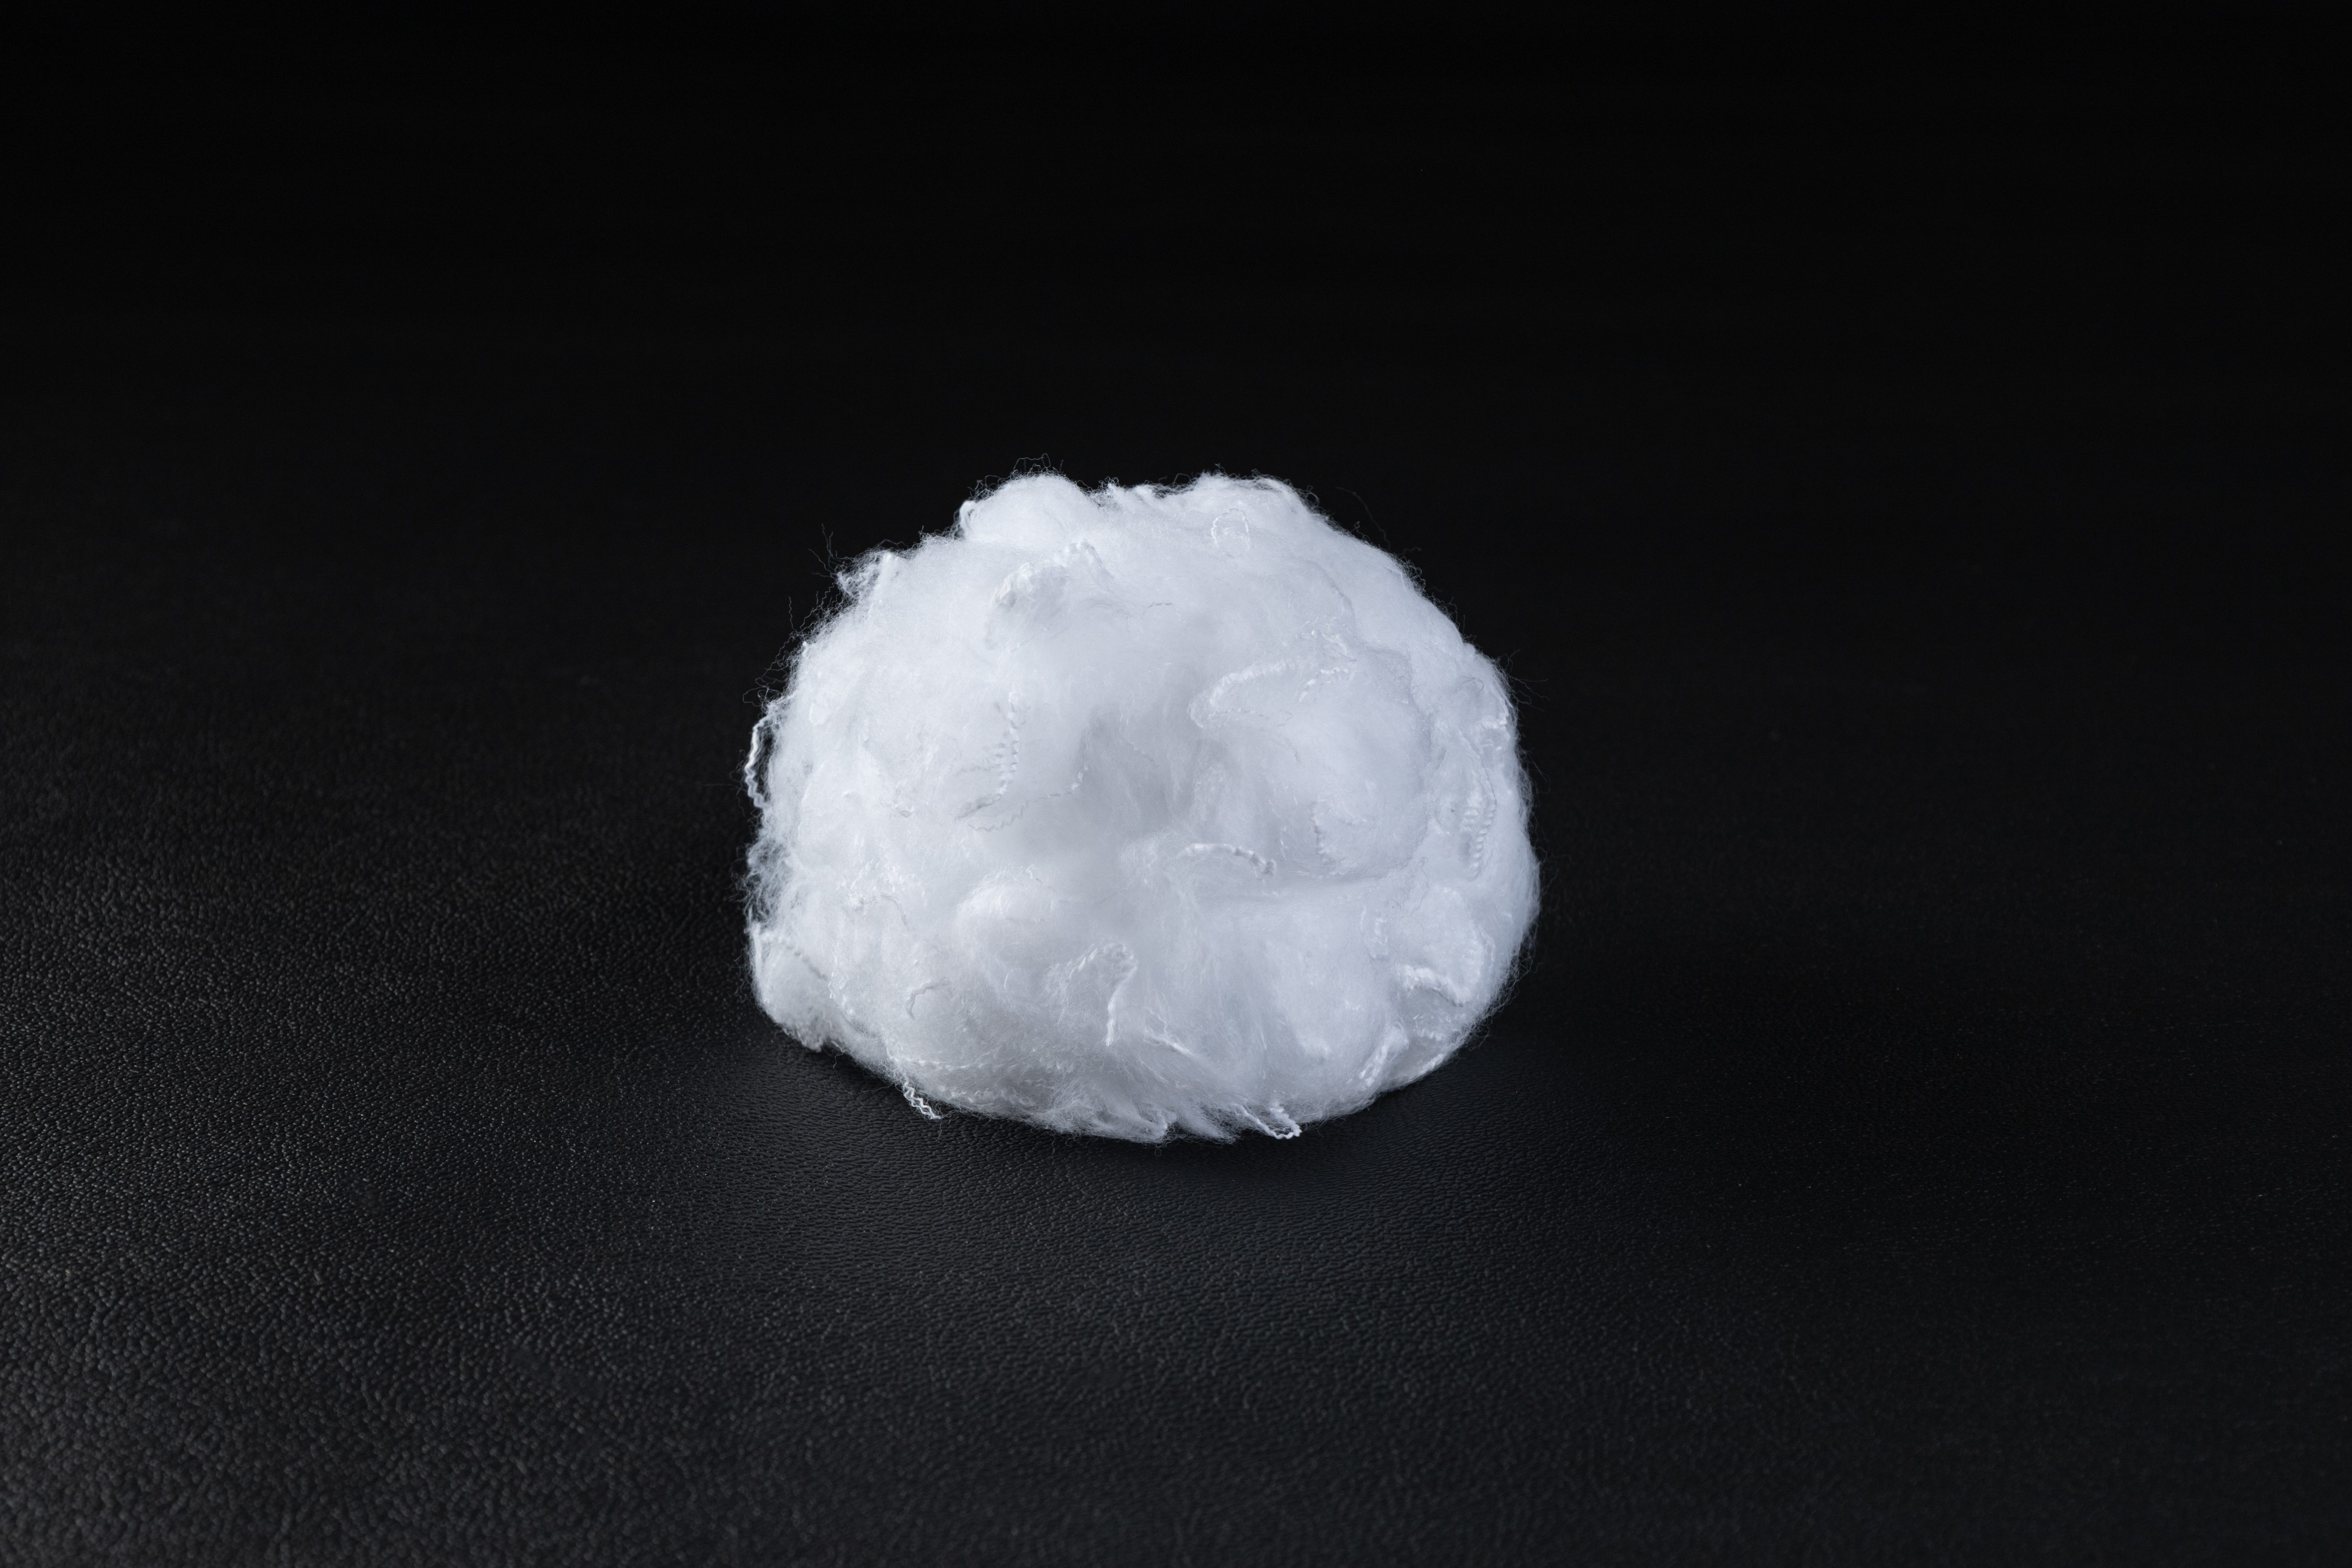
Modern binder fibers utilize a core-sheath bicomponent structure to achieve targeted bonding. The core typically consists of standard polyester (PET), which maintains its solid state up to 250°C. The sheath consists of a modified copolymer (Co-PET) or polyethylene (PE) engineered to melt at a significantly lower temperature. The sheath's melting point acts as the thermal trigger. As the web passes through the oven, the sheath melts and forms adhesive droplets. The core remains solid, acting as a structural pillar. This dual-action mechanism is exactly why Nonwoven Low Melt Fiber maintains web integrity while providing robust adhesion. Concentric configurations ensure even polymer distribution around the core, while eccentric configurations can induce natural crimp during heating, adding extra loft to the final product.
Differential Scanning Calorimetry (DSC) is the industry-standard method for verifying melting behavior. A DSC curve maps the heat flow into the fiber as temperature increases, providing a thermal fingerprint of the polymer. Operators look for the glass transition temperature (Tg) and the peak melting temperature (Tm). The onset temperature shows exactly when the sheath begins to soften, which dictates the start of your processing window. Relying on a single melting point number on a spec sheet is risky. The DSC curve reveals the entire melting behavior. A broad endothermic peak indicates a wide, forgiving processing window. A sharp peak requires highly precise oven zone calibration to prevent sudden polymer degradation.
DSC Curve Metric | Technical Definition | Impact on Production Line |
|---|---|---|
Onset Temperature | The point where the polymer first begins to absorb heat and soften. | Dictates the minimum temperature the first oven zone must reach to initiate bonding. |
Peak Melting Temperature (Tm) | The temperature at which the maximum rate of melting occurs. | Represents the target core temperature the web must achieve for optimal sheath flow. |
Endset Temperature | The point where the melting process is completely finished. | Exceeding this temperature rapidly decreases polymer viscosity, risking web shrinkage. |
Peak Width | The temperature range between onset and endset. | A wider peak allows for faster line speeds and less precise oven controls. |
The thickness of the fiber directly interacts with its melting point and the required thermal energy. Denier dictates the surface area-to-volume ratio of the individual filament. Finer deniers, such as 2D or 3D, heat rapidly. They melt faster and require precise oven calibration to prevent the sheath from degrading before the web exits the heating zone. Coarser deniers, such as 6D or 15D, possess greater mass. They require longer dwell times or higher thermal energy to achieve proper sheath flow. When mixing different deniers in a single blend, you must adjust the through-air oven speed to accommodate the slowest-heating fiber. Failure to account for denier variations results in surface melting, where the outside of the web bonds but the core remains loose and unbonded.
The 110°C melting point is the industry workhorse for thermal bonding. The chemical composition relies on modified Co-PET. Manufacturers add specific monomers like isophthalic acid or diethylene glycol to the polymer chain during synthesis to disrupt crystallization. This effectively lowers the melting point from the standard 250°C of pure PET down to 110°C. This range offers an excellent balance of bond strength, fabric flexibility, and energy efficiency. Best use cases include general wadding, furniture upholstery, mattress manufacturing, and standard apparel insulation. The 110°C threshold allows for rapid line speeds in standard drum ovens without risking thermal damage to common matrix fibers like standard polyester or nylon.
Achieving higher melting points requires a distinct shift in polymer chemistry. The Co-PET is engineered with higher crystallinity and fewer chain disruptors. This prevents the resulting bonds from softening during secondary processing or high-temperature end-use. You need low melt fiber for nonwovens in this range for abrasive or high-heat environments. Best use cases include automotive trunk liners, industrial abrasive pads, and materials undergoing secondary heat treatments like thermoforming, molding, or deep-draw pressing. If the end product will sit in a hot warehouse, a commercial dryer, or a vehicle interior under direct sunlight, a 130°C to 150°C binder ensures the fabric will not lose its dimensional stability or delaminate.
Ultra-low melt fibers typically utilize Polyethylene (PE) or Polypropylene (PP) sheaths rather than modified polyesters. These polyolefins naturally melt at much lower temperatures. Best use cases involve highly heat-sensitive substrates. Natural fibers like cotton, wool, or delicate viscose will scorch, yellow, or become brittle at higher temperatures. Specialized hygiene products also rely heavily on sub-100°C binders. The lower temperature preserves the ultra-soft hand feel required for skin-contact applications, as PE remains highly flexible even after melting and cooling. Processing these fibers requires strict temperature controls, as overshooting the narrow melting window will cause the web to collapse into a rigid, plastic-like sheet.
The nonwovens industry is rapidly adopting recycled low melt fibers to meet sustainability targets. However, rPET introduces specific thermal variables that operators must manage. Impurities in the recycled feedstock, varying intrinsic viscosity, and mixed polymer origins can cause slight fluctuations in the melting point curve. A batch of rPET binder might show a melting peak at 108°C instead of the expected 110°C, or it might exhibit a much broader DSC peak. These minor shifts require wider processing windows in your oven settings. Stricter quality assurance testing is mandatory. You must run DSC tests on incoming bales of recycled fiber to adjust your line speed and prevent inconsistent bonding across the width of the web.
Melting Point Range | Sheath Chemistry | Primary Applications | Thermal Processing Window |
|---|---|---|---|
Sub-100°C | Polyethylene (PE) / Polypropylene (PP) | Hygiene, Medical, Delicate Natural Fibers | Narrow (Requires precise control) |
110°C | Modified Co-PET | Apparel, Upholstery, Mattress Wadding | Broad (Highly forgiving) |
130°C - 150°C | High-Crystalline Co-PET | Automotive, Abrasives, Thermoforming | Moderate (Requires higher energy) |
Filtration media demands high porosity, precise pore size retention, and structural rigidity under pressure. The binder cannot impede the airflow or fluid dynamics of the filter. You need a filter material bonding fiber that melts cleanly at the intersections without spreading excessively across the matrix fibers, which would blind the filter media. Filtration environments are inherently harsh. Hot gases, automotive fluids, and industrial liquid filtration systems operate at elevated temperatures and high pressures. Therefore, filtration media often requires specific melting points above 130°C. This prevents bond degradation, media migration, and chemical breakdown when the filter is deployed in the field.
Automotive OEMs enforce stringent requirements for thermal stability, acoustic performance, and flammability. Insulation near the engine bay or exhaust system faces constant extreme heat. Cabin acoustics require flame retardant compatibility and long-term loft retention to absorb sound waves effectively. You must evaluate the trade-off between using a 110°C versus a 150°C melt point. A 110°C binder saves energy during manufacturing but may fail the OEM's long-term dimensional stability tests under a hot car roof in summer climates. A 150°C binder ensures the acoustic panels maintain their loft, rigidity, and sound-absorbing properties over the vehicle's entire lifespan.
Medical and hygiene textiles prioritize an ultra-soft hand feel, rapid liquid strike-through, and high-speed production capabilities. Diaper acquisition distribution layers (ADL), feminine care products, and medical absorbent pads cannot feel stiff or abrasive against the skin. Lower melting points are preferred here. PE sheaths melt quickly and remain highly flexible after cooling. This prevents the formation of rigid, scratchy bond points that cause skin irritation. Furthermore, the lower processing temperatures ensure the primary matrix fibers retain their natural softness and capillary action. Biocompatibility in skin-contact applications is non-negotiable, making pure PE/PET bicomponent fibers the standard choice for these sectors.
The relationship between the fiber's melting point, oven dwell time, and web throughput speed dictates your daily yield. A lower melting point allows the sheath to reach its flow state faster. This increases production capacity and reduces bottlenecking at the thermal bonding stage. However, pushing the oven temperature too high to force a faster line speed will degrade the polymer and cause surface glazing. You must map the exact dwell time required for the convective heat to penetrate the core of the web. Surface heating is useless if the center remains unbonded. Operators must balance the air velocity in through-air ovens with the target melting point to ensure uniform heat distribution.
Matching binder melt points to matrix fibers requires a strict decision framework to prevent destroying your raw materials. The golden rule is maintaining a minimum 20°C buffer between the binder's melting point and the matrix fiber's degradation point.
Identify the maximum temperature the primary matrix fiber can withstand before shrinking, yellowing, or losing tensile strength.
Subtract 20°C to 30°C from that maximum temperature to establish your absolute ceiling for the oven.
Select a binder fiber with a peak melting temperature that falls safely below that ceiling.
Run a small-scale test to verify that the matrix fiber does not stiffen during the required dwell time.
If your matrix fiber is standard PET melting at 250°C, a 110°C binder is perfectly safe. If you are mixing low melt PET with cotton, wool, or viscose, you must respect the natural fiber's scorch point. Cotton begins to yellow around 150°C. Therefore, utilizing a 110°C or sub-100°C binder is mandatory. Ignoring substrate compatibility results in brittle, discolored, and unsellable fabric.
The viscosity of the melted sheath at specific temperatures dictates the final fabric feel and drape. If the oven is set exactly at the melting point, the polymer remains highly viscous. It forms small, flexible bond points at the exact intersections. The fabric remains soft and pliable. If the oven exceeds the melting point by 15°C to 20°C, the polymer viscosity drops significantly. It flows aggressively, coating the matrix fibers and creating large, rigid intersections. This drastically increases the stiffness of the final product. You must control the melt viscosity through precise temperature zoning to achieve the desired rigidity for industrial pads or the desired flexibility for apparel.
The chosen melting point directly affects the end product's lifecycle durability and resistance to secondary processing. Fabrics subjected to consumer washing, commercial dry cleaning, or industrial calendering face repeated thermal and mechanical stress. A 110°C binder may soften during high-temperature commercial laundering or steam pressing, causing the fabric to lose structural loft and become flat. For heavy-duty applications, a 130°C or 150°C thermal bonded polyester fiber provides superior resistance to post-processing degradation. The bonds remain intact, ensuring the nonwoven material performs consistently over years of heavy use.
Exceeding the optimal melting window is a primary failure mode in nonwoven production. When the oven is too hot, the sheath flows too much, draining away from the fiber intersections and pooling in the web. This creates brittle bonds, reduces fabric loft, and causes severe web shrinkage. The matrix fibers pull together as the liquid polymer contracts during cooling. Mitigation requires strict oven profiling. You must run data loggers through your oven to verify the exact temperature in every zone. Regular calibration of thermocouples is essential. Utilizing fibers with a wider thermal processing window also provides a safety margin against minor temperature spikes.
Insufficient heat penetration in thick, high-gsm webs creates a layered failure. The surface fibers reach the melting point and bond perfectly, creating a crust. The core of the web does not reach the activation temperature. The resulting fabric suffers from delamination, splitting apart under minimal tension. Mitigation involves adjusting the dwell time and optimizing web density before it enters the oven. Utilizing forced-air through-bond ovens ensures convective heat reaches the core rapidly. Alternatively, selecting a binder with a sharper melting curve ensures that once the core reaches temperature, bonding occurs instantly without requiring prolonged exposure.
Ultra-low melt fibers face unique logistical challenges before they even reach the production line. Fibers with sub-100°C melting points can begin to fuse or clump in non-climate-controlled warehouses during peak summer months. This phenomenon, known as blocking, renders the bales unusable. The fibers will not open properly in the bale breaker or carding machine, leading to massive defects. Mitigation requires implementing strict inventory temperature controls. Warehouses must be ventilated and cooled. You must enforce strict FIFO (First-In, First-Out) stock rotation for highly sensitive binder fibers to minimize their exposure to seasonal heat waves. Limit stacking heights to reduce pressure on the bottom bales, which accelerates blocking.
Specifying a higher melting point than necessary drives up continuous energy costs. Heating an industrial oven to 160°C requires significantly more natural gas or electricity than heating it to 130°C. This unnecessarily inflates your carbon footprint and operational overhead. Mitigation involves conducting rigorous cost-benefit analyses. Compare your daily energy consumption against the actual required thermal stability of the end product. Do not over-engineer the bond. Select the lowest possible melting point that still meets the lifecycle durability requirements of the final application.
Production Defect | Root Cause | Immediate Corrective Action |
|---|---|---|
Web Shrinkage / Glazing | Oven temperature exceeds the endset melting point. | Reduce zone temperatures by 5°C increments; increase line speed. |
Core Delamination | Insufficient dwell time for heat to penetrate the web core. | Decrease line speed; increase forced air velocity in the oven. |
Poor Tensile Strength | Oven temperature is below the peak melting point. | Increase zone temperatures; verify thermocouple accuracy. |
Fiber Clumping at Carding | Premature activation (blocking) during warehouse storage. | Isolate affected bales; implement climate control in storage areas. |
The suitable melting point for your production line is a calculated intersection of matrix fiber thermal limits, oven capabilities, and end-product environmental exposure. Start with the maximum temperature the end product will face in its lifecycle. Add a 20°C safety margin. Select the lowest possible melting point above that threshold to optimize manufacturing costs and line speeds.
Request technical data sheets (TDS) and DSC curves from your fiber supplier to verify exact melting windows.
Procure sample bales of different deniers and melting points for initial testing.
Conduct pilot line trials to map actual oven dwell times and heat penetration in your specific web density.
Perform tensile and loft recovery tests on the pilot fabric before committing to full-scale procurement.
A: The standard melting point is 110°C. This utilizes a modified Co-PET sheath. It provides an optimal balance of energy efficiency, rapid line speeds, and strong adhesion for general applications like wadding, upholstery, and apparel insulation.
A: Select a melting point based on the filter's operating environment. Industrial filters handling hot gases or automotive fluids require 130°C to 150°C binders to prevent bond degradation. Ensure the melt viscosity allows for precise pore size retention.
A: Yes. A 110°C binder is safe for cotton and wool. These natural fibers generally scorch or yellow at temperatures above 150°C. The 110°C melting point provides a sufficient thermal buffer to prevent substrate damage during oven processing.
A: Overheating causes the sheath polymer to liquefy completely and flow away from fiber intersections. This results in brittle bonds, severe loss of fabric loft, web shrinkage, and potential thermal degradation of the primary matrix fibers.
A: Finer deniers have a higher surface area-to-volume ratio, allowing them to heat and melt rapidly. Coarser deniers possess more mass and require longer oven dwell times or higher temperatures to achieve the same level of sheath melt flow.
A: Co-PET sheaths typically melt between 110°C and 150°C, offering strong, durable bonds for industrial and apparel use. PE sheaths melt below 100°C, providing an ultra-soft, flexible hand feel ideal for hygiene and delicate skin-contact applications.
A: Store ultra-low melt fibers in climate-controlled, well-ventilated warehouses. Prevent exposure to direct sunlight and extreme summer heat to avoid blocking (clumping). Implement strict First-In, First-Out (FIFO) inventory rotation to minimize storage duration.